What Are The Different Aluminum Extrusion Profiles
Updated: 12 Sep 2023
What is aluminum extrusion profile
Aluminum extrusion profiles are manufactured by forcing a heated aluminum billet through a specially designed steel die. The die determines the cross-sectional shape, allowing manufacturers to produce simple sections as well as complex profiles with grooves, ribs, channels, and internal cavities.Common shapes include L, U, T, and H profiles, round and rectangular tubes, and custom-designed sections.
After extrusion, the profiles undergo cooling, stretching when required, cutting, and aging according to the alloy and temper specification. Additional processes such as anodizing, powder coating, and CNC machining may be applied depending on the final application.
Unlike components made by bending or machining, extruded aluminum profiles can integrate several functional features into one continuous cross-section.
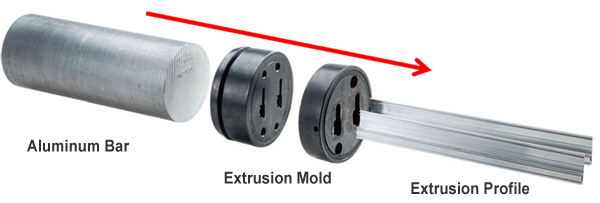
Solid, Hollow and Semi-Hollow Aluminum Extrusions
Aluminum extrusion profiles are commonly divided into three categories based on their cross-sectional geometry: solid, hollow, and semi-hollow.
These differences affect not only the profile's appearance but also die design, manufacturing difficulty, and potential applications.
Solid Aluminum Extrusion Profiles
Solid profiles do not contain fully enclosed cavities. Examples include aluminum angles, flat bars, T-profiles, and many open channels.
They are generally produced using solid dies, which are often less complex than the dies required for hollow sections.
However, extrusion difficulty still depends on profile dimensions, wall thickness, and cross-sectional balance. Wide, thin sections or deep projections may require special attention during die design.
Solid extrusions are commonly used for brackets, mounting rails, edge protection, and connecting components.
Hollow Aluminum Extrusion Profiles
Hollow profiles contain one or more fully enclosed cavities.
Examples include round tubes, rectangular tubes, multi-chamber frames, and certain structural extrusions.
Complex hollow profiles are commonly manufactured using porthole or bridge dies, where aluminum flows around internal supports and rejoins inside the die.
Hollow sections can provide a useful balance between weight and structural stiffness. However, their actual load-bearing capacity depends on geometry, alloy, temper, and loading conditions.
Profiles with multiple narrow chambers or thin internal walls may require more complex tooling and tighter control of metal flow.
Semi-Hollow Aluminum Extrusion Profiles
Semi-hollow profiles have partially enclosed cross-sections, such as deep grooves with relatively narrow openings.
Some mounting channels, guide profiles, and interlocking sections fall into this category.
Although they may look similar to solid profiles, their geometry can create difficult-to-support die features.
Increasing the opening width or adjusting internal radii may improve manufacturability without significantly affecting the intended function.
Extrusion Profile vs Aluminum Extrusion vs Other Aluminum Forming Methodse
Aluminum components can be manufactured using extrusion, sheet metal bending, roll forming, casting, and CNC machining.Each process has different advantages depending on the required geometry, production volume, dimensional accuracy, and material properties.
|
Manufacturing Method |
Main Characteristics |
Suitable Applications |
|---|---|---|
|
Extrusion |
Produces continuous, complex cross-sections |
Frames, channels, tubes, custom profiles |
|
Sheet Metal Bending |
Forms sheet into angles and folded shapes |
Covers, brackets, panels |
|
Roll Forming |
Forms continuous profiles from sheet through rollers |
Certain channels and sheet-based sections |
|
Casting |
Produces complex three-dimensional components |
Housings, brackets, mechanical parts |
|
CNC Machining |
Removes material to achieve precise features |
Precision parts, holes, slots, mating surfaces |
Extrusion is particularly useful when a component requires the same cross-section along its length.
For example, an aluminum window frame can incorporate glazing channels, sealing grooves, and reinforcement features in one extruded section.
However, extrusion does not automatically provide higher dimensional accuracy than other manufacturing methods. Accuracy depends on the process, tooling, material, geometry, and tolerance requirements.
For components requiring precision holes, threads, or localized features, extrusion can be combined with CNC machining.
Aluminum Extrusion Profile Features
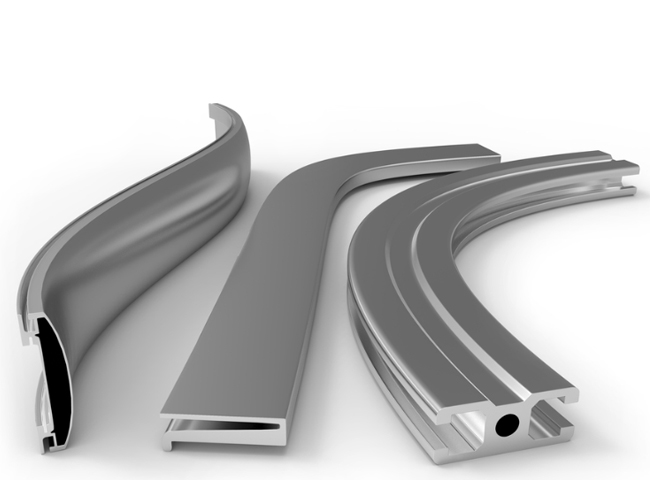
Extruded aluminum profiles can be customized to a great extent based on customer requirements and specific application needs, offering variations in terms of shape, dimensions, materials, surface treatments, and usage.Profile shape: Extruded aluminum profiles can be manufactured in various shapes, including angle aluminum, round tubes, square tubes, T-profiles, H-profiles, U-profiles, cylinders, and more. Different shapes are suitable for different application requirements.
Beyond standard L, U, T, and H sections, aluminum extrusion allows multiple functional features to be integrated into a single profile.
For example, an industrial framing profile may combine fastening slots, internal cavities, and reinforcement ribs. An architectural profile may include channels for glass, seals, or other accessories.
The most suitable shape depends on the required assembly method, loading conditions, and manufacturing feasibility.
Profile dimensions: Extruded aluminum profiles can be customized to different dimensions according to customer needs, including length, width, thickness, and other aspects.
Profile dimensions should be evaluated together with wall thickness, cross-sectional geometry, and dimensional tolerances.
For custom aluminum extrusions, dimensions such as groove width, internal clearance, wall thickness, and mating surfaces may be more critical than the overall width and height.
A profile with excessive thickness variation may also be more difficult to extrude consistently.
Aluminum alloy materials:
Different aluminum alloys offer different combinations of strength, extrudability, corrosion resistance, and finishing performance.
Common extrusion alloys include 6063, 6061, 6005A, and 6082.
- 6063: Frequently used for architectural and decorative profiles due to its good extrudability and finishing characteristics.
- 6061: Commonly selected for structural and machined components requiring higher mechanical strength.
- 6005A: Used in various structural profiles, including support frames and solar mounting applications.
- 6082: Suitable for many higher-strength structural applications.
The appropriate alloy should be selected according to the profile's geometry, mechanical requirements, surface finish, and production conditions.
The specified temper, such as T5 or T6, also affects the final mechanical properties.
Surface treatments: Extruded aluminum profiles can undergo various surface treatments such as anodizing, painting, electrophoretic coating, powder coating, etc., to provide different appearances and durability.
The selection of surface treatment should consider both appearance and operating conditions.
Anodizing is often suitable for architectural and decorative aluminum profiles, while powder coating offers a wide range of colors and protective finishes.
For components with narrow slots or close-fitting connections, coating thickness should be considered during dimensional design.
Usage: Different extruded aluminum profiles are suitable for various application fields, such as construction, automotive manufacturing, aerospace, electronics, furniture manufacturing, etc. Therefore, the profile's usage also influences its design and manufacturing requirements. Profiles used in architectural applications may prioritize appearance, corrosion resistance, and assembly compatibility.
Industrial profiles may place greater emphasis on stiffness, dimensional consistency, and machining requirements.
The same basic profile shape may therefore require different alloys, tolerances, or finishes depending on its intended use.
How Profile Geometry Affects Aluminum Extrusion
The cross-sectional geometry of an aluminum profile directly affects extrusion feasibility, dimensional stability, and manufacturing cost.Even when two profiles use the same alloy, differences in wall thickness, cavities, and internal features can lead to different production challenges.
Wall Thickness Distribution
Relatively uniform wall thickness generally helps maintain balanced metal flow during extrusion.
Large differences between thick and thin sections can contribute to uneven flow, distortion, and dimensional variation.
Where possible, designers should avoid unnecessary thickness changes and use gradual transitions between sections.
However, minimum feasible wall thickness depends on the alloy, profile size, die design, and extrusion equipment. There is no single minimum thickness suitable for every aluminum extrusion.
Internal Corners and Radii
Sharp internal corners can create difficulties in die manufacturing and metal flow.
Suitable radii may improve die strength and reduce stress concentration.
The radius must also remain compatible with the component's assembly requirements.
Grooves, Ribs and Hollow Chambers
Deep grooves, narrow openings, and thin internal ribs increase profile complexity.
For hollow sections, additional chambers may improve functional performance but also increase tooling difficulty.
These features should be evaluated during die development rather than after the tooling has been completed.
Profile Symmetry
Symmetrical cross-sections often make balanced metal flow easier to achieve.
Asymmetrical sections can still be extruded, but they may require adjustments to die bearing lengths and other tooling features.
An early review of the profile drawing can help identify geometry that may cause unnecessary manufacturing difficulties.
Dimensional Tolerances of Aluminum Extrusions
Dimensional tolerances define the acceptable variation between the specified drawing dimensions and the manufactured aluminum profile.Important tolerance requirements include:
- Cross-sectional dimensions: Width, height, wall thickness, and groove dimensions.
- Straightness: Deviation along the length of the profile.
- Twist: Rotation of the cross-section along its length.
- Angularity: Deviation between specified surfaces.
- Cut length: Permitted variation in the finished length.
Standards such as EN 755-9 and ANSI H35.2 provide dimensional tolerance references for applicable aluminum extrusion products.
However, the required tolerances should be selected according to the specific application.
For example, a decorative aluminum trim may not require the same dimensional control as a precision mounting profile.
When certain holes, slots, or mating surfaces require tighter accuracy than extrusion can economically provide, secondary CNC machining may be appropriate.
Clearly identifying critical dimensions on the drawing can help reduce unnecessary manufacturing costs.
What Affects Aluminum Extrusion Cost?
The cost of aluminum extrusion depends on material consumption, tooling complexity, production quantity, and additional processing requirements.Profile Weight
Weight per meter is one of the main factors affecting material cost.
For aluminum with an approximate density of 2.70 g/cm³:
Weight (kg/m) ≈ Cross-sectional area (mm²) × 0.0027
For example, if a profile has a cross-sectional area of 500 mm²:
500 × 0.0027 = 1.35 kg/m
This is a theoretical weight calculation. Actual weight varies with alloy density and dimensional tolerances.
Die Complexity
Simple solid profiles generally require less complicated tooling than multi-chamber hollow profiles of comparable size.
Additional cavities, deep grooves, and thin internal features can increase die development difficulty.
Alloy and Temper
Different alloys have different extrusion characteristics, while temper requirements affect subsequent processing.
Order Quantity
Production quantity influences the allocation of tooling, setup, and testing costs.
Finishing and Machining
Anodizing, powder coating, cutting, drilling, tapping, and CNC milling add manufacturing steps.
For this reason, reducing profile weight does not always reduce the total cost if the design becomes substantially more difficult to manufacture.
How to Select an Aluminum Extrusion Profile
Choosing the right aluminum extrusion profile requires consideration of both the intended function and manufacturing requirements.Before selecting a standard profile or developing a custom cross-section, buyers and engineers should confirm the following information:
- Application: Is the profile used for structural support, framing, mounting, guiding, or decoration?
- Cross-sectional geometry: Does the design require open channels, hollow cavities, internal ribs, or connection features?
- Alloy and temper: What mechanical properties, corrosion resistance, and finishing characteristics are required?
- Dimensions and tolerances: Which dimensions are critical for assembly or performance?
- Secondary processing: Will the profile require cutting, drilling, tapping, bending, or CNC machining?
- Surface finish: Is anodizing, powder coating, or another finish required?
- Order quantity: Is the project intended for prototype development or batch production?
It allows the manufacturer to review wall thickness, die feasibility, dimensional requirements, and potential manufacturing challenges before tooling begins.
Shenghai Aluminum provides custom aluminum extrusion manufacturing, including die development, surface finishing, cutting, and CNC machining.
Customers can submit profile drawings, alloy requirements, surface finishes, and estimated quantities for technical review and quotation.